SuperMotors SuperMotors SUPERMOTORS Search: try “orange Bronco on 35s”
Home/ Registry/ Ford/ Bronco/ 1992-1996/ “Wookie”/ Photo supermotors.net/registry/media/1138897

When welding sheet metal, its best to use the TIG. But, since I…
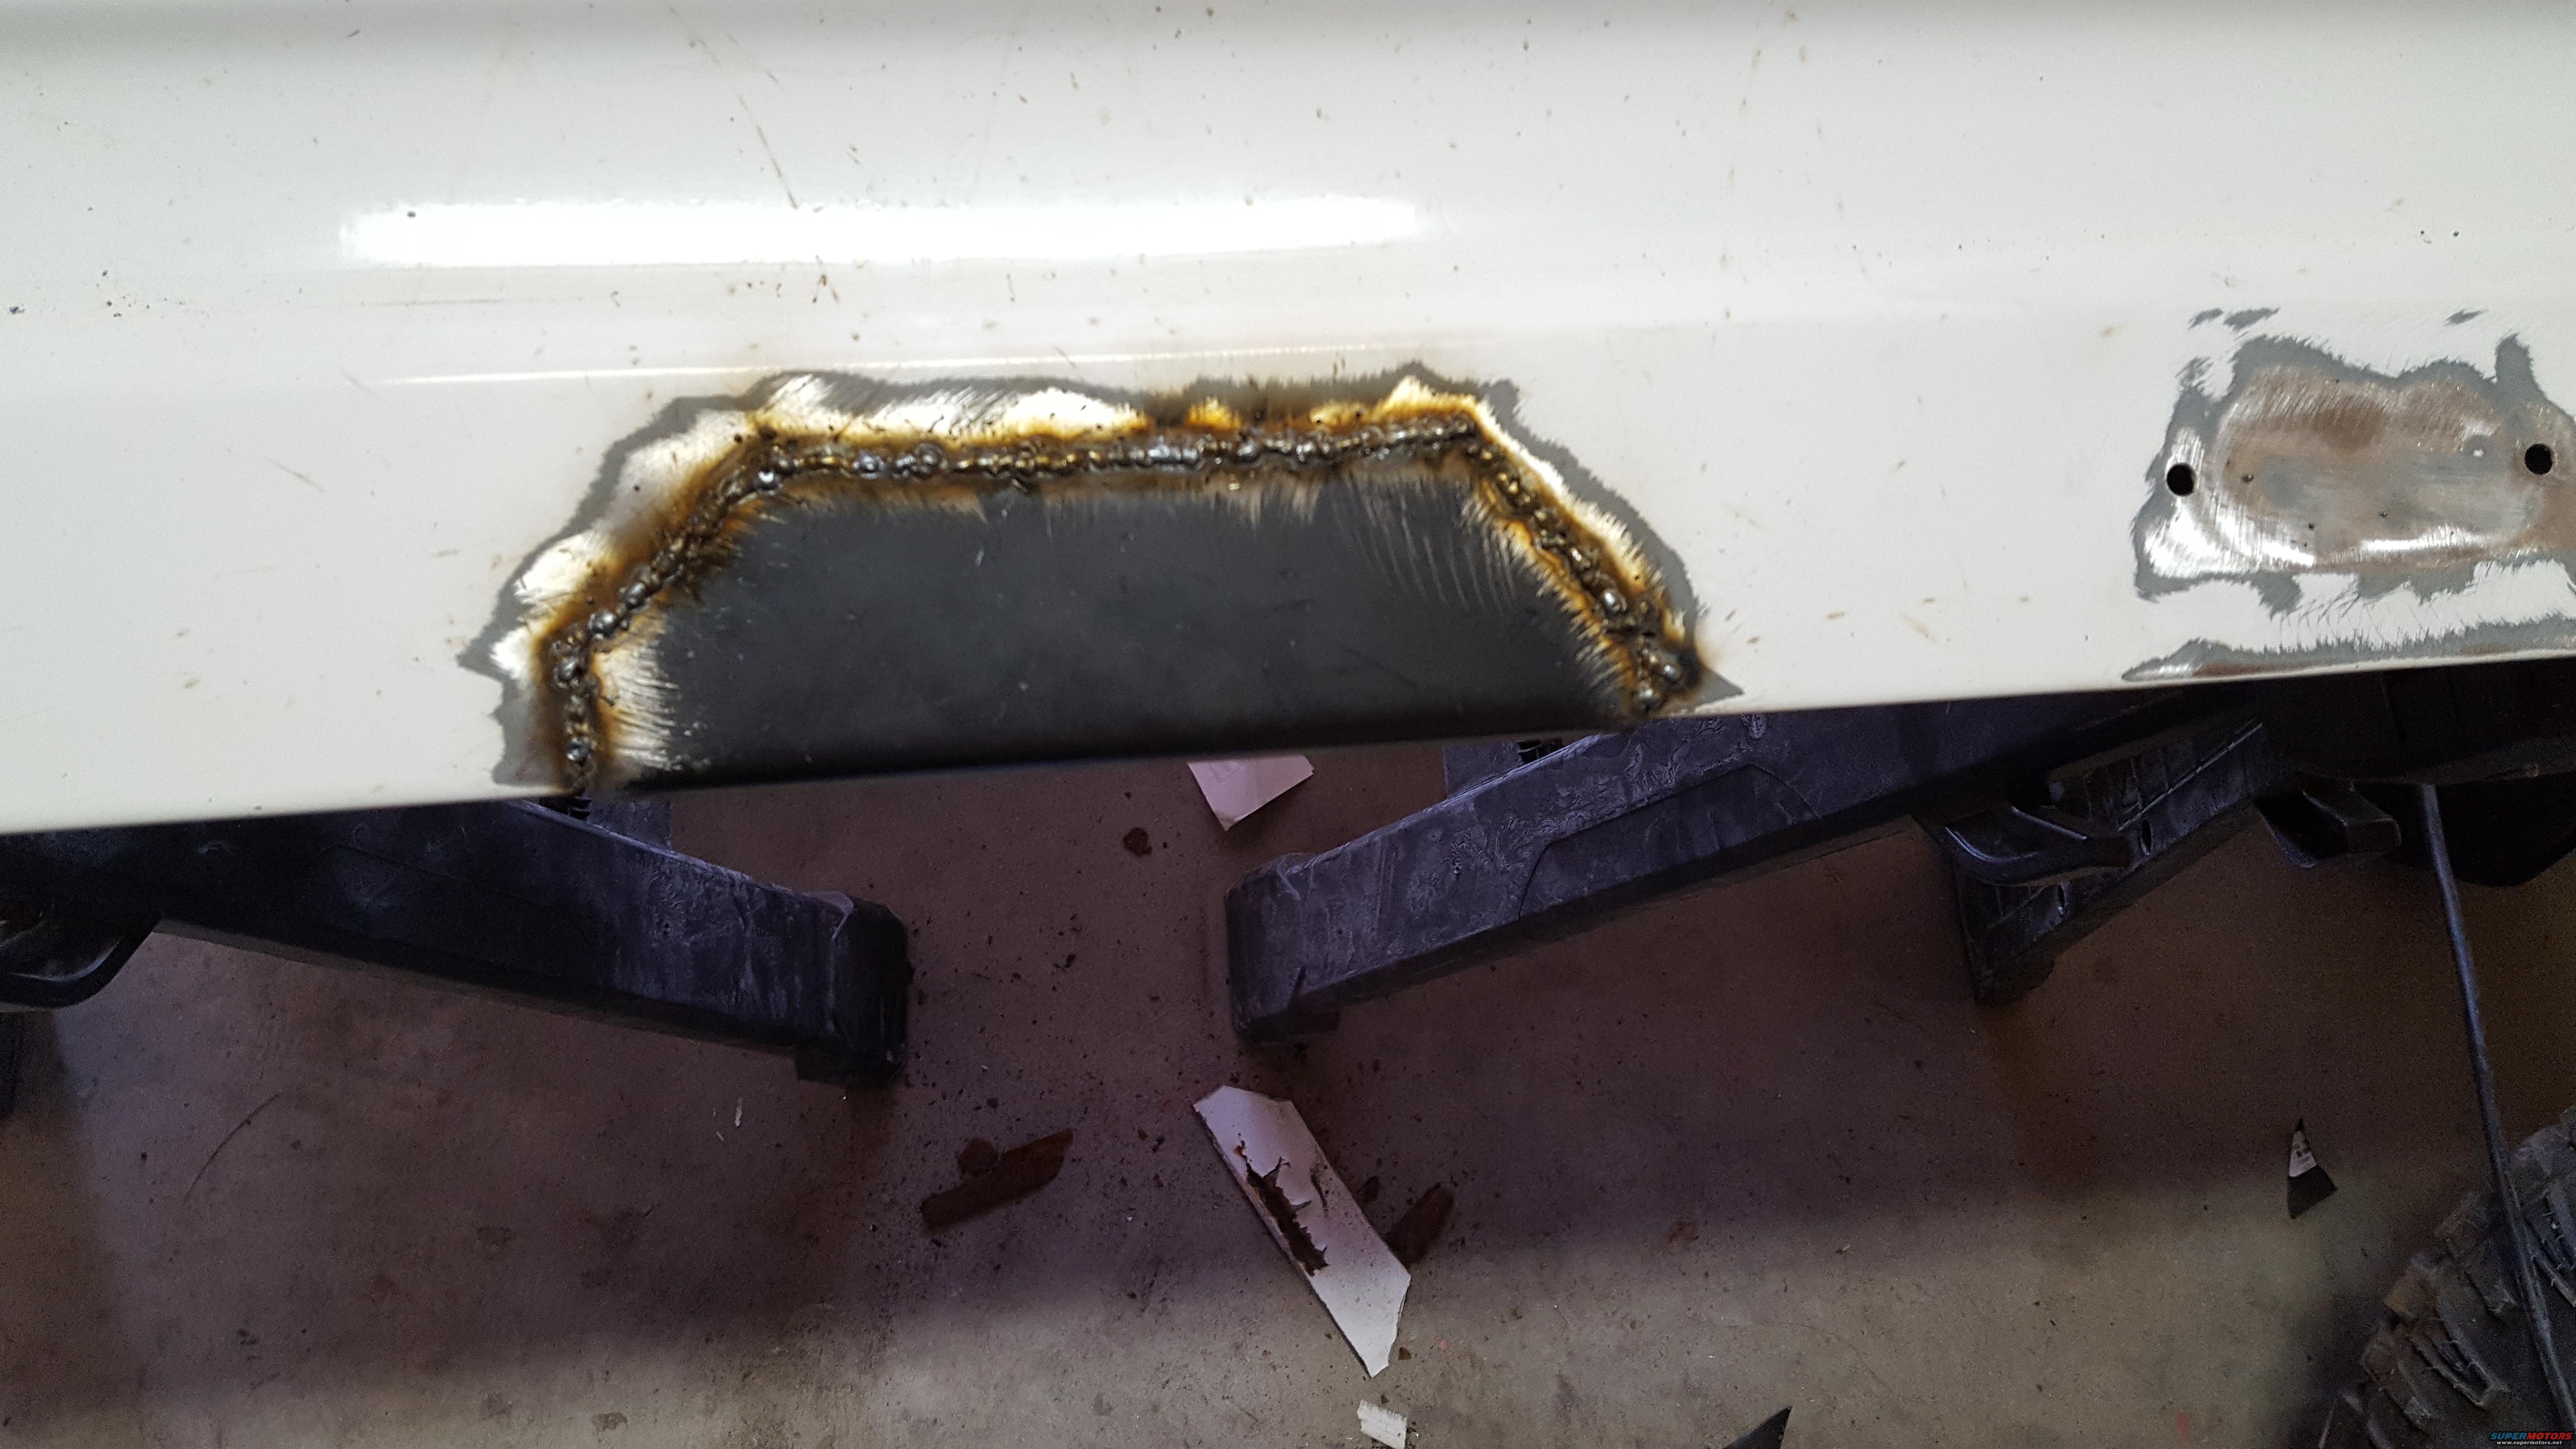
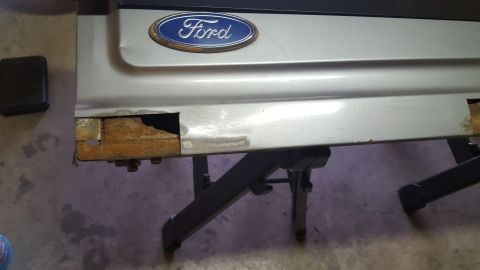
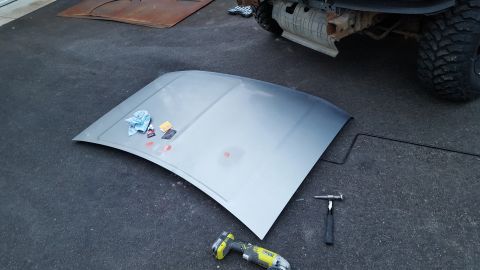
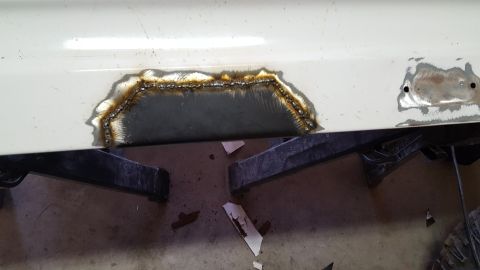
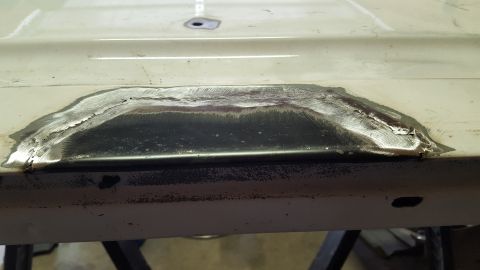
When welding sheet metal, its best to use the TIG.  But, since I don't have any Argon at the moment, and I have plenty of 75/25 on hand, it'll get MIG'ed.

Mig welding mild steel in gauges this thin is not rocket science, but can be tricky.  The key here is not to build up too much heat, or the metal will warp.

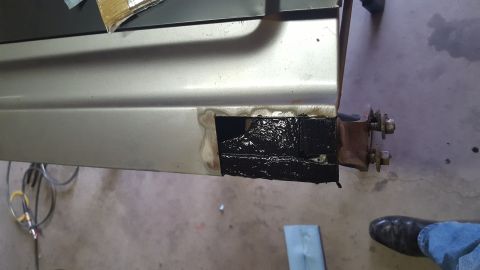
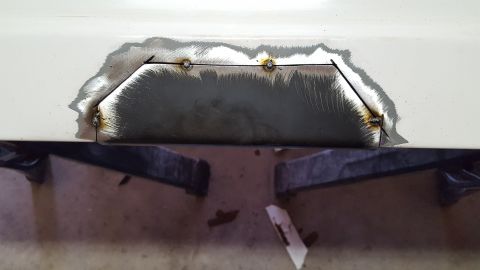
In order to keep the heat down I played "connect the dots" here.  I'd make a tack weld, wait 'till it cooled, and proceeded to make another.  I also moved around a lot in order for the heat to dissipate.

What you wind up with is this really ugly-looking weld, but its flat.  If you try to MIG it shut the normal way, the weld will look much better, but you'll have a wavy piece of metal.

On the welder settings, we want to be a little 'hot'.  Since we're not making a continuous bead, and since we want enough penetration, we'll configure the MIG to be a little on the hot side.
When welding sheet metal, its best to use the TIG. But, since I don't have any Argon at the moment, and I have plenty of 75/25 on hand, it'll get MIG'ed. Mig welding mild steel in gauges this thin is not rocket science, but can be tricky. The key here is not to build up too much heat, or the metal will warp. In order to keep the heat down I played "connect the dots" here. I'd make a tack weld, wait 'till it cooled, and proceeded to make another. I also moved around a lot in order for the heat to dissipate. What you wind up with is this really ugly-looking weld, but its flat. If you try to MIG it shut the normal way, the weld will look much better, but you'll have a wavy piece of metal. On the welder settings, we want to be a little 'hot'. Since we're not making a continuous bead, and since we want enough penetration, we'll configure the MIG to be a little on the hot side.Original file
When welding sheet metal, its best to use the TIG.  But, since I don't have any Argon at the moment, and I have plenty of 75/25 on hand, it'll get MIG'ed.

Mig welding mild steel in gauges this thin is not rocket science, but can be tricky.  The key here is not to build up too much heat, or the metal will warp.

In order to keep the heat down I played "connect the dots" here.  I'd make a tack weld, wait 'till it cooled, and proceeded to make another.  I also moved around a lot in order for the heat to dissipate.

What you wind up with is this really ugly-looking weld, but its flat.  If you try to MIG it shut the normal way, the weld will look much better, but you'll have a wavy piece of metal.

On the welder settings, we want to be a little 'hot'.  Since we're not making a continuous bead, and since we want enough penetration, we'll configure the MIG to be a little on the hot side.

When welding sheet metal, its best to use the TIG. But, since I don't have any Argon at the moment, and I have plenty of 75/25 on hand, it'll get MIG'ed.

Mig welding mild steel in gauges this thin is not rocket science, but can be tricky. The key here is not to build up too much heat, or the metal will warp.

In order to keep the heat down I played "connect the dots" here. I'd make a tack weld, wait 'till it cooled, and proceeded to make another. I also moved around a lot in order for the heat to dissipate.

What you wind up with is this really ugly-looking weld, but its flat. If you try to MIG it shut the normal way, the weld will look much better, but you'll have a wavy piece of metal.

On the welder settings, we want to be a little 'hot'. Since we're not making a continuous bead, and since we want enough penetration, we'll configure the MIG to be a little on the hot side.

Owner caption · Photo 38 of 76

Is this accurate? Sign in to help verify it.
Comments

No comments yet.

More 1992-1996 Broncos