Home/
Registry/
Ford/
Bronco/
1987-1991/
1989 Ford Bronco/
Photo
supermotors.net/registry/media/615165
Multi-Pass Fillet Weld Sketch - 3-Pass Bead Sizes & Sequence Diagram

Reference · 1987-1991 BroncoAll 95 service procedures
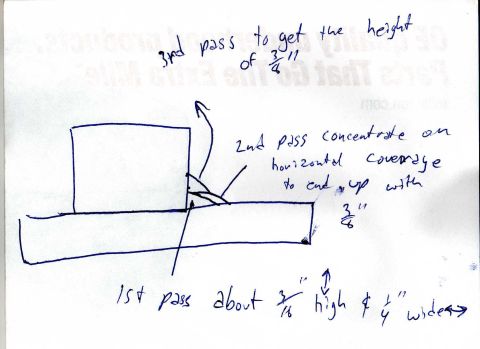

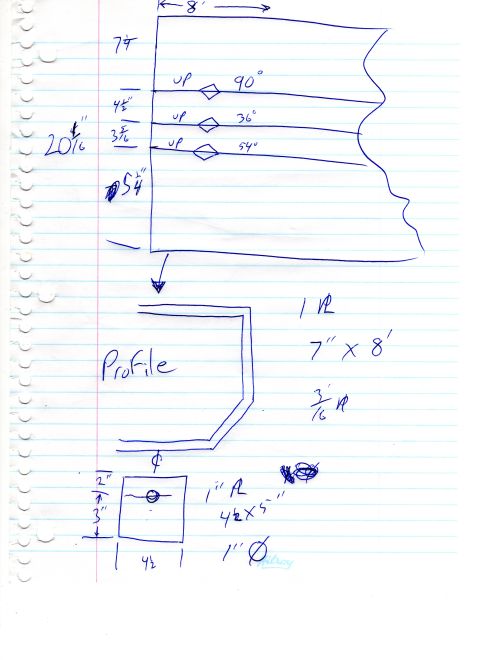







Freehand sketch describing a three-pass welding procedure to build up a part to a target height and width.
Part of 1987-1991 Ford Bronco Service Procedures
This document is a hand-drawn, handwritten sketch illustrating a multi-pass fillet weld procedure for joining a vertical plate to a horizontal plate at a T-joint. The drawing shows two rectangular pieces of material meeting at roughly a right angle, with the weld built up in three passes at the joint. Annotations with arrows explain the sequence and target dimensions: the 1st pass is laid at the root of the joint and should be about 3/16 inch high and 1/4 inch wide; the 2nd pass concentrates on horizontal coverage across the base plate so the weld ends up 3/8 inch wide; and the 3rd pass builds vertical height to achieve a total weld height of 3/4 inch. Small directional arrows clarify which dimensions are height versus width. A reader can learn a basic three-pass stacking strategy for a large fillet weld, root pass first, then a horizontal spreading pass, then a vertical height pass, along with approximate bead size targets for each pass. The sketch contains no vehicle-specific information, part numbers, dates, or torque values; it appears to be a personal shop note likely related to fabrication or repair work documented in the uploader's vehicle gallery.
Is this accurate? Sign in to help verify it.
Frequently asked questions
- How many weld passes does this fillet weld procedure use?
- Three passes: a 1st root pass, a 2nd pass for horizontal coverage, and a 3rd pass to build height.
- How big should the first weld pass be?
- The 1st pass should be about 3/16 inch high and 1/4 inch wide.
- What is the purpose of the second pass?
- The 2nd pass concentrates on horizontal coverage so the weld ends up 3/8 inch wide.
- What is the third pass for and what final height does it achieve?
- The 3rd pass builds the weld to get a final height of 3/4 inch.
- What kind of joint is shown in the sketch?
- A T-style joint with a vertical plate sitting on a horizontal plate, welded with a multi-pass fillet weld at the corner.






No comments yet.